Industrial Membrane Systems

Messinger Engineering develops membrane filtration systems for product separation, purification, concentration and process optimization.
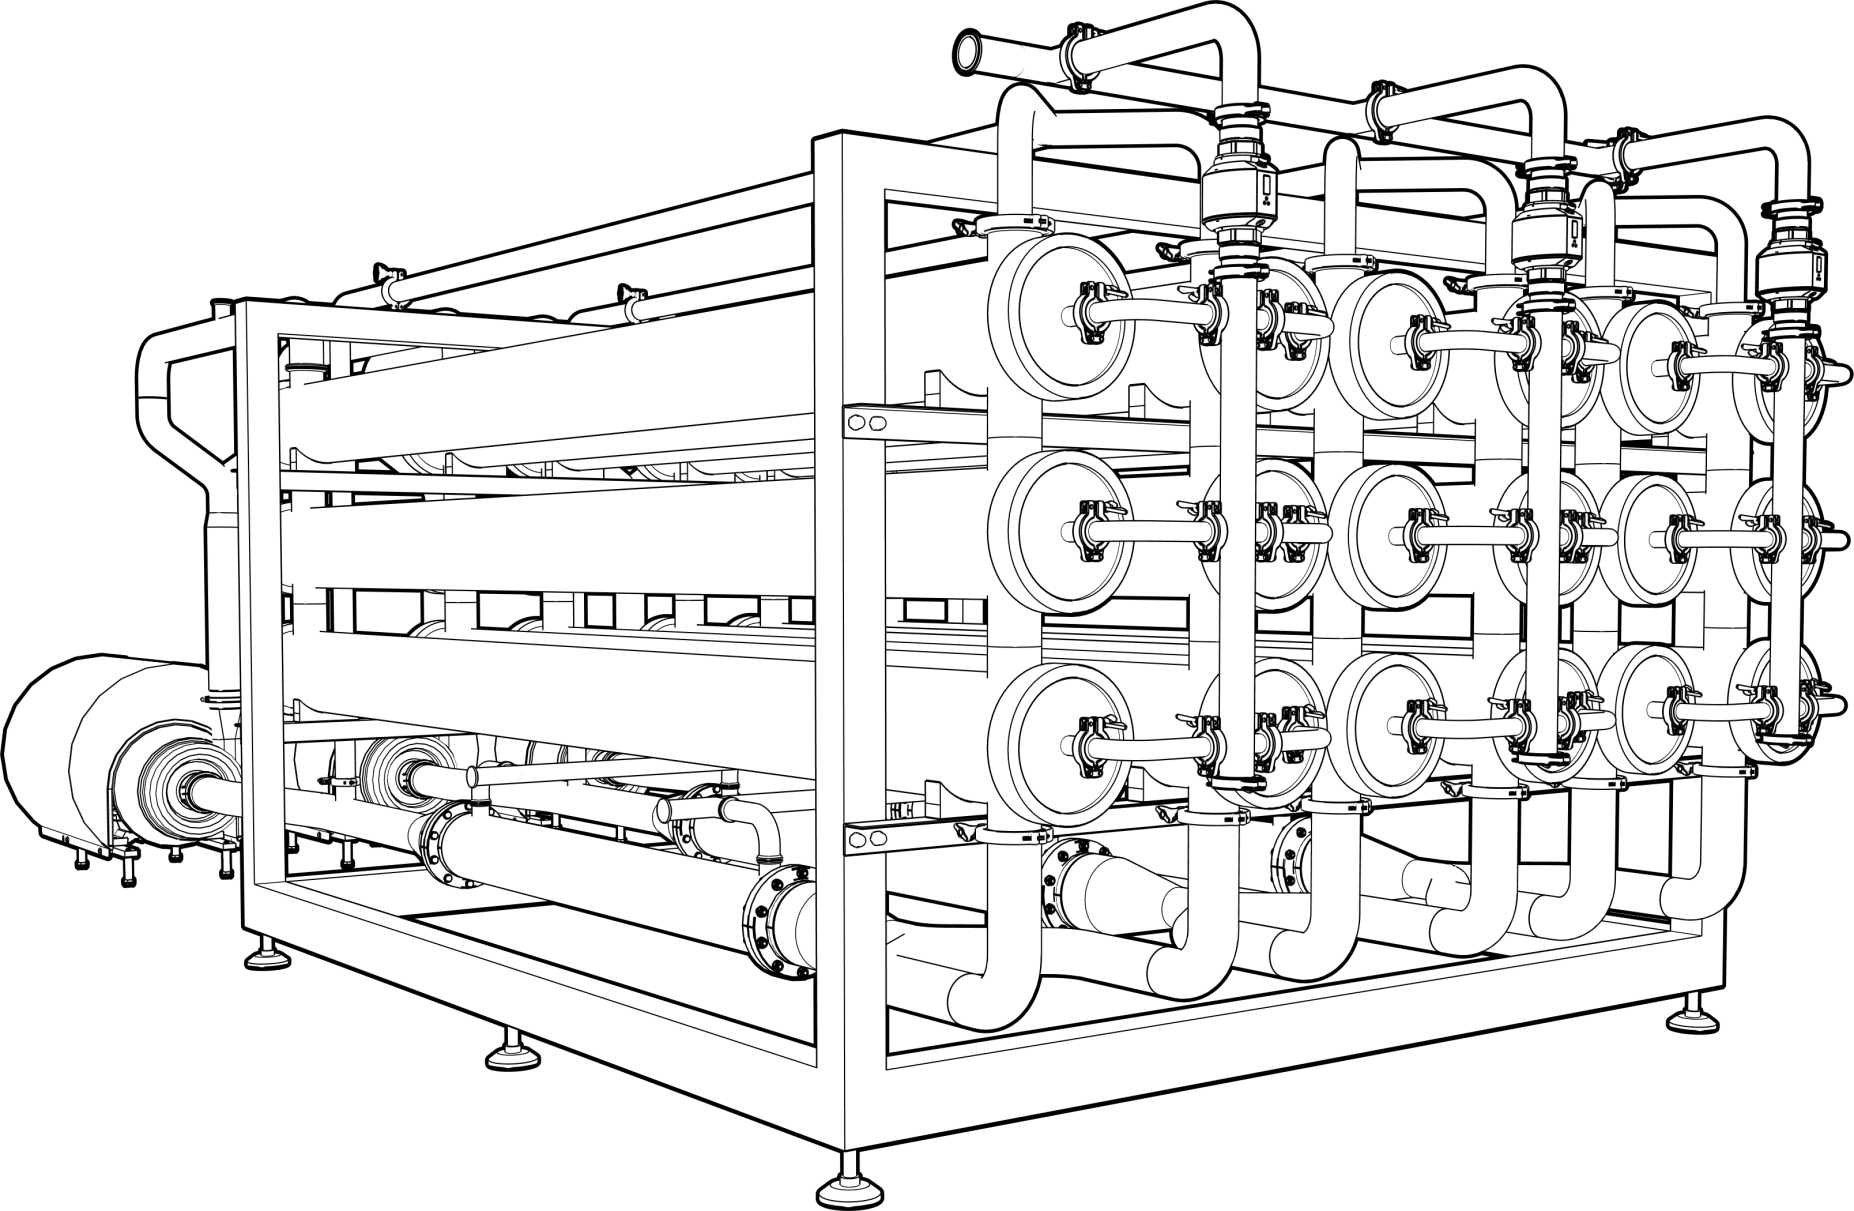
Industrial membrane filtration system for process engineering, pilot plants and scale-up

We engineer modular, intelligent membrane systems for demanding food and biotech applications. From laboratory and pilot systems to fully automated production equipment — engineered for hygienic design, food-grade operation and ASME BPE requirements. Clever. Compact. Built for what comes next.

We provide the engineering foundation for reliable industrial operation.

We Think in Systems.
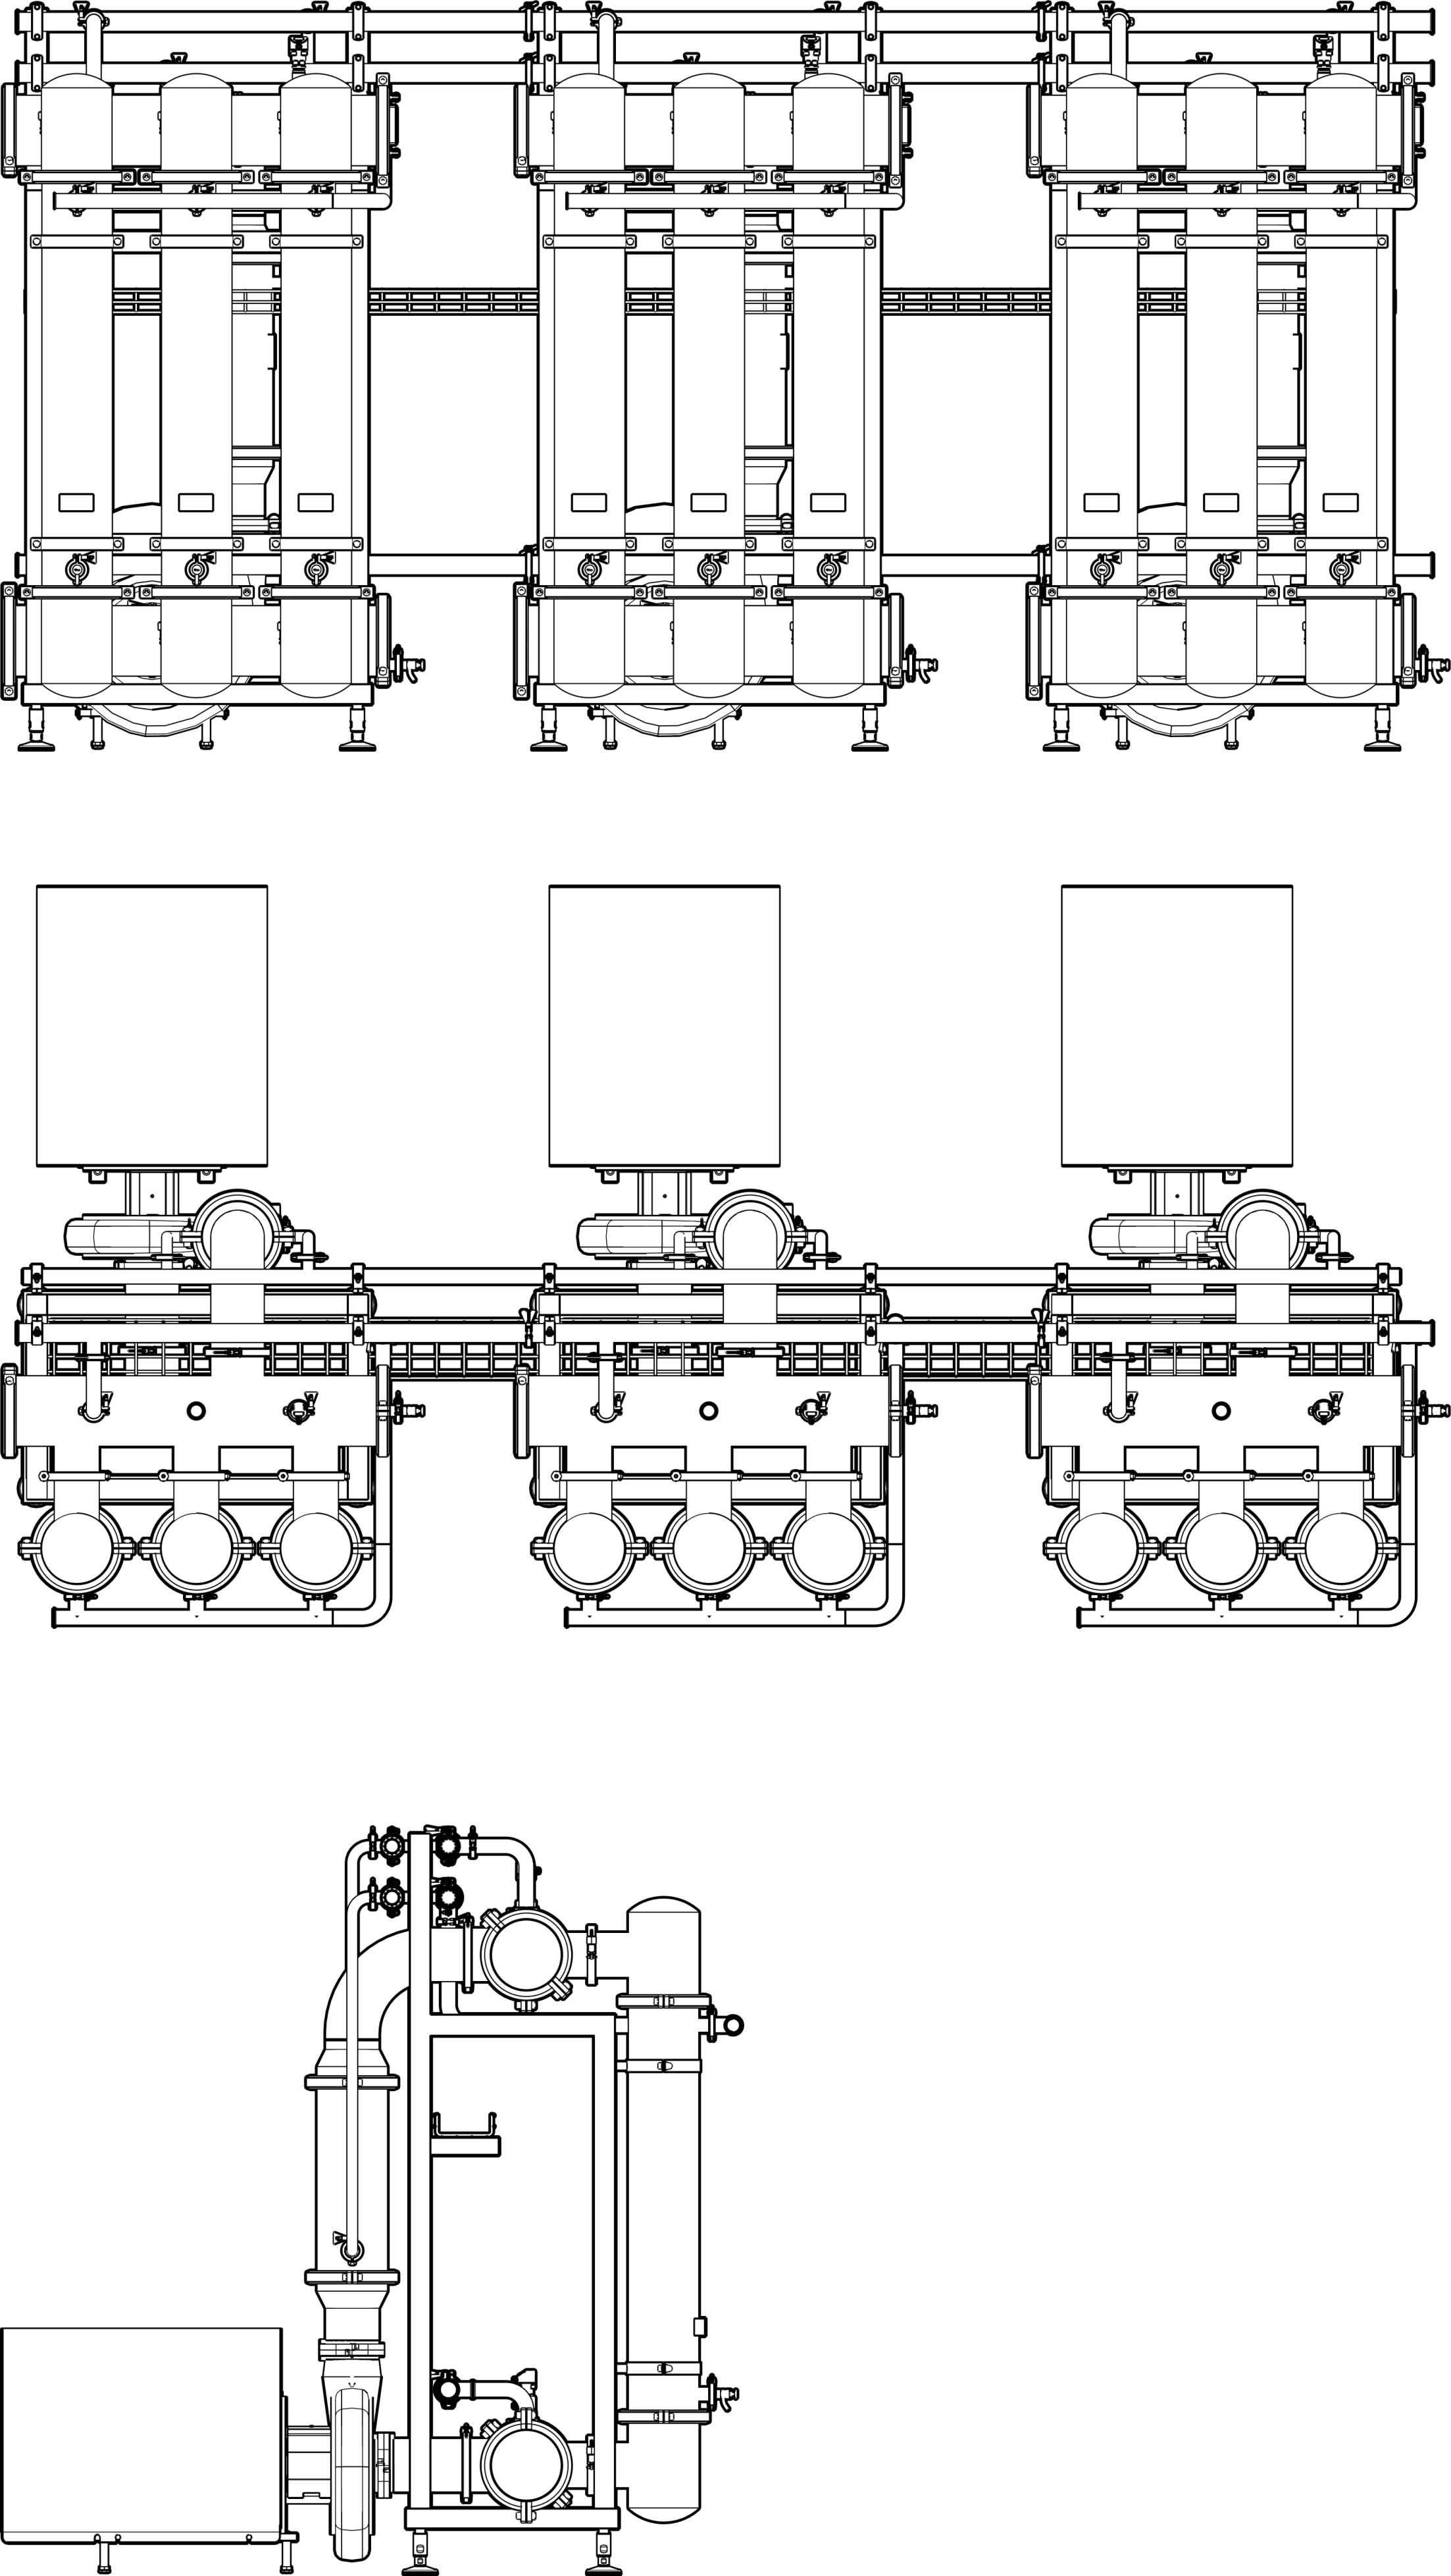
We think in systems

Every pump influences the separation performance. Every valve influences cleaning. Every sensor influences operation. A membrane system works as a whole.

That is why we engineer systems, not assemblies of individual components. Components, modules and functions are designed to work together — and to be exchanged, extended or adapted when requirements change.

Standardised interfaces, modular design and ASME BPE and food-grade components create flexibility without unnecessary complexity. The result is a compact, maintainable system that can evolve with new membranes, applications, instrumentation and automation.
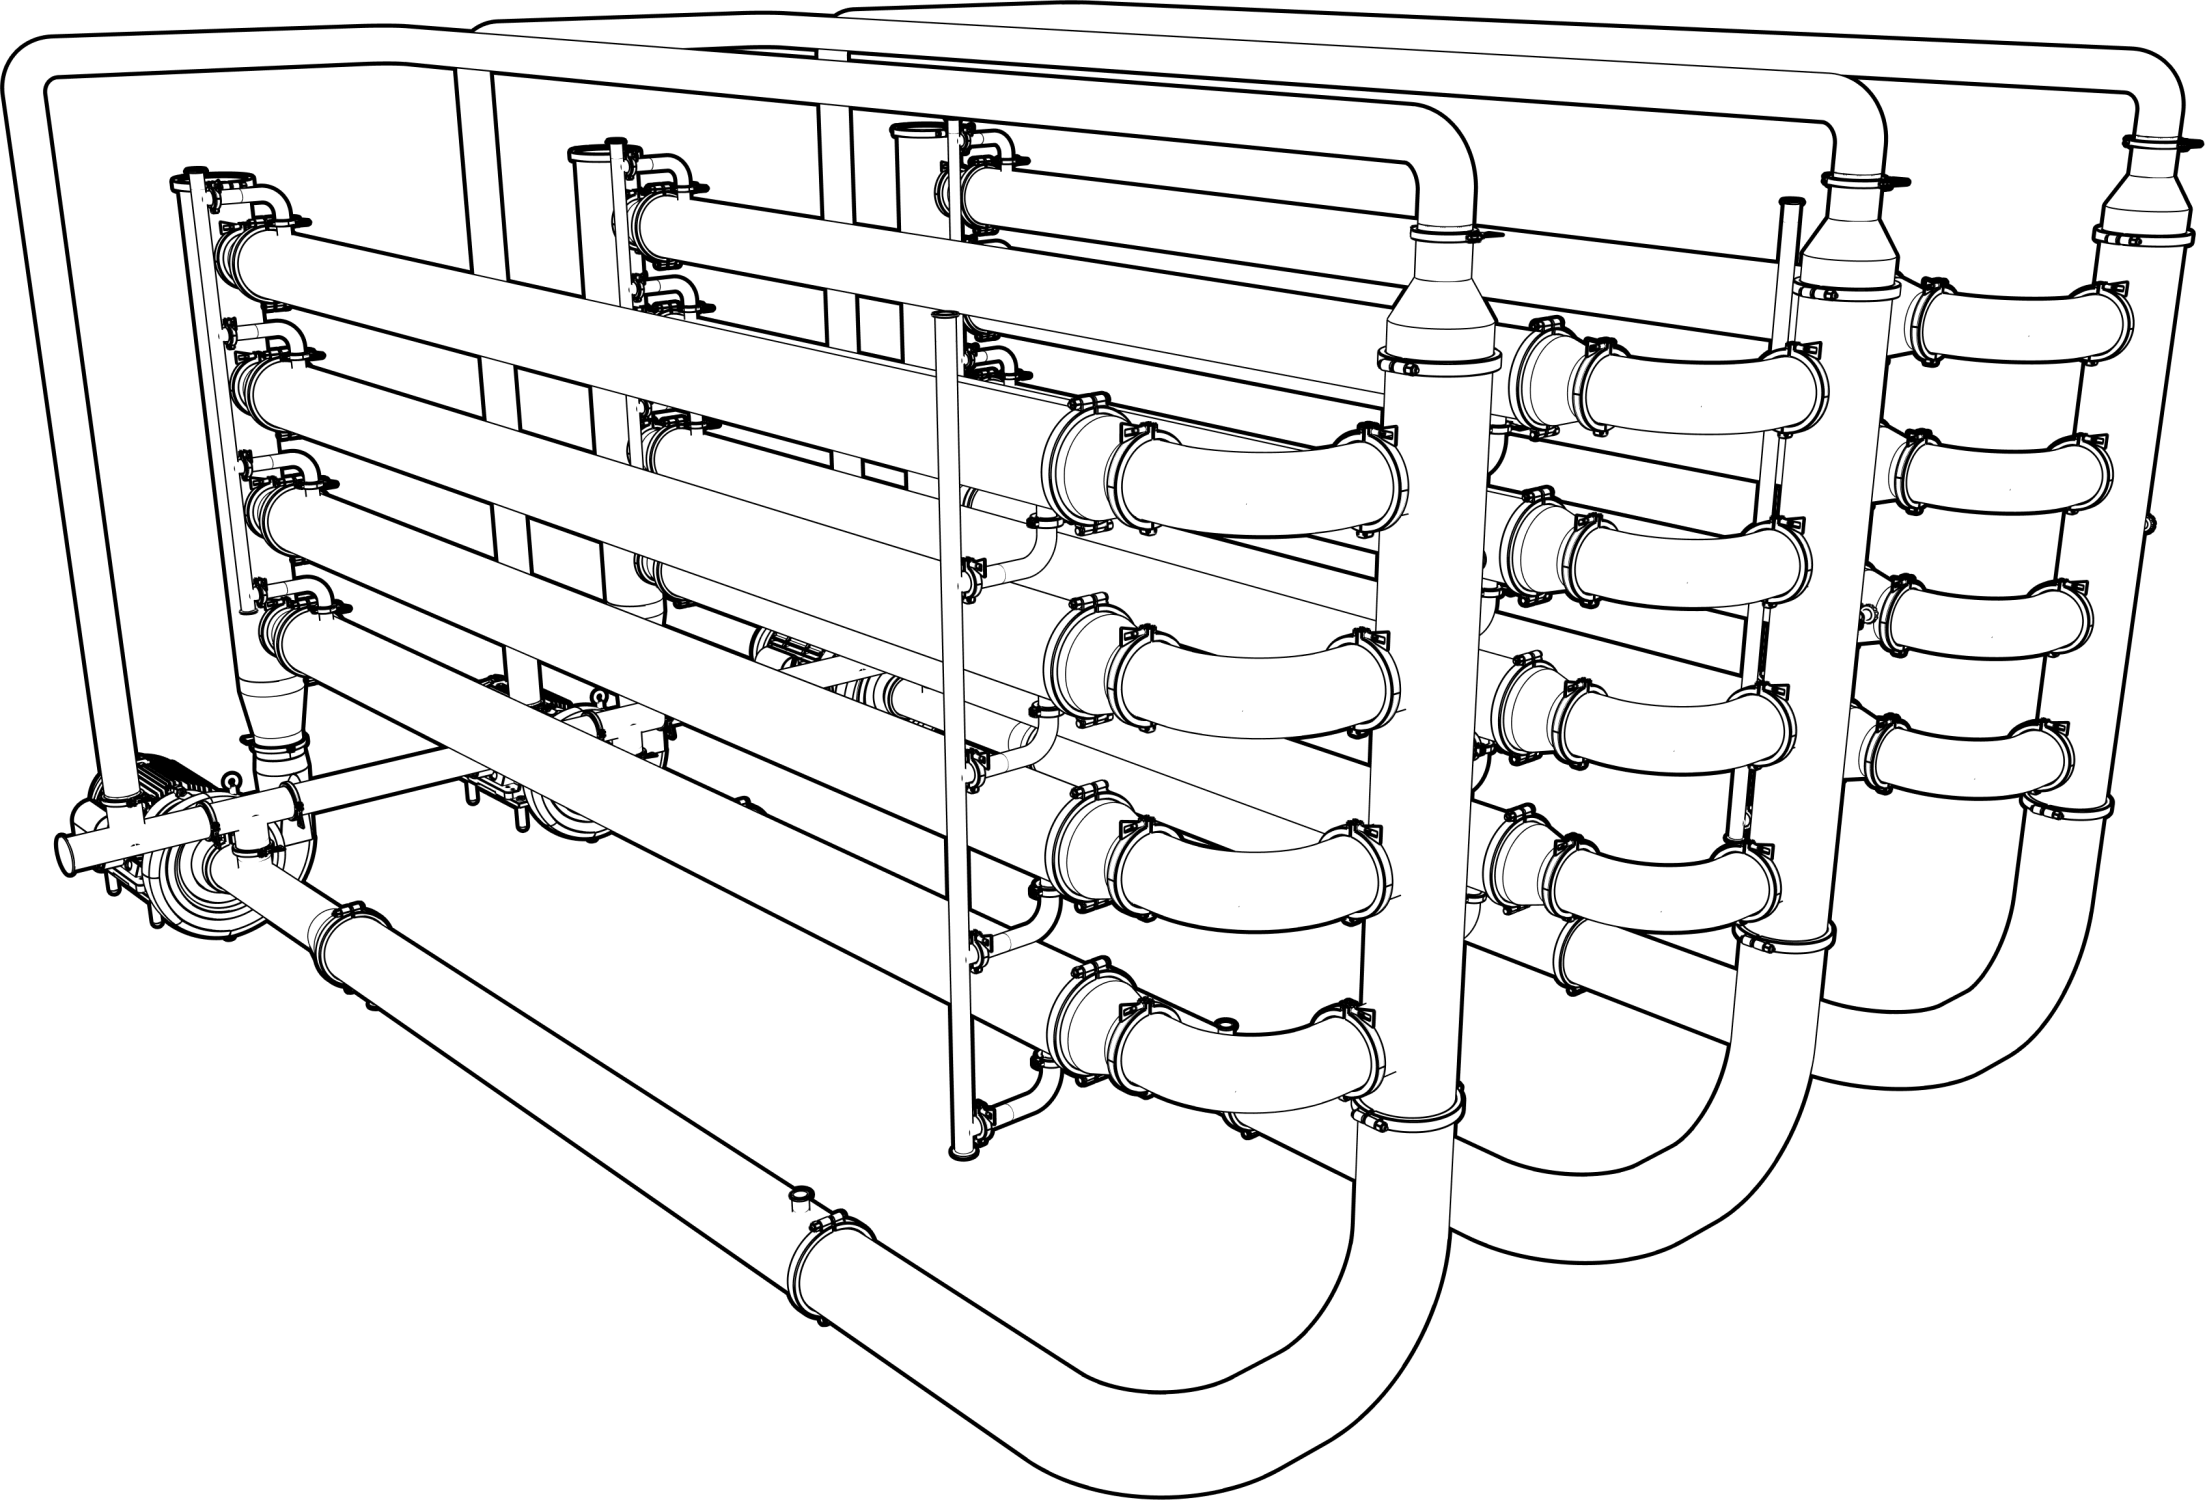
Tubular

Not a collection of over-specified equipment. A coherent engineering system, built for today and ready for what comes next.

ASME BPE provides internationally recognised engineering principles for hygienic equipment and piping systems. We apply these principles to membrane systems where cleanability, hygienic design, materials, surface finishes, connections and drainability are critical.
Learn more about ASME BPE →
Clever automation starts with the people who operate the system. We combine engineering experience, operator and process-owner knowledge, AI-assisted software development and open-source technologies to create lean, transparent and adaptable control systems — built to evolve rather than become obsolete.
Membrane systems for fermentation broths, biomass separation, product recovery, concentration and downstream processing.
Robust ceramic membrane systems for demanding feeds, high temperatures, aggressive cleaning conditions and applications requiring high durability.
Ceramic Membranes →
Cleaning and CIP concepts engineered as an integral part of the membrane system for effective cleaning, reproducibility and hygienic operation.
Membrane systems for protein concentration, fractionation, clarification, diafiltration and recovery in dairy and protein processing.
Controlled diafiltration systems for washing, purification and removal of low-molecular-weight components from concentrated products.
Hygienic membrane systems for clarification, concentration, fractionation, product recovery and water reuse in food processing.
Food-grade materials, hygienic components and cleanable system layouts designed for safe and practical production environments.
Compact, modular membrane systems engineered for reliable industrial operation, maintainability and future adaptation.
Membrane systems for recovering valuable proteins, ingredients and functional components from process streams and side streams.
Flexible laboratory systems for membrane screening, parameter studies, concentration, diafiltration and generation of scale-up data.
Microfiltration systems for clarification, particle removal, cell separation and pretreatment of complex process streams.
Standardised interfaces and modular system architecture allow components, membrane stages and functions to be exchanged, extended or adapted.
Nanofiltration systems for selective separation, concentration, demineralisation and purification of liquid process streams.
Pilot systems that bridge laboratory development and industrial implementation under representative operating conditions.
Reverse osmosis systems for concentration, water recovery, desalination and high-quality process water applications.
Translation of laboratory and pilot data into membrane area, hydraulic design, equipment sizing and industrial system architecture.
Ultrafiltration systems for clarification, protein concentration, macromolecule separation and processing of challenging feed streams.
Membrane systems for process-water treatment, water reuse, wastewater reduction and recovery of valuable components.

Why Messinger Engineering?

Engineering begins with understanding the process. The equipment follows.

Our projects begin with laboratory experiments, continue through pilot-scale validation and lead to reliable industrial production. This development strategy reduces technical risk while generating the process knowledge required for successful implementation.

Whether the application involves food processing, dairy, biotechnology, fermentation, ingredient recovery, water treatment or specialty chemical separations, our objective remains the same: develop membrane processes that work reliably — not only in the laboratory, but for years in industrial production.